From Local Supplier to Global OEM Partner: How OLANTAI Supports Private Label Programs Worldwide
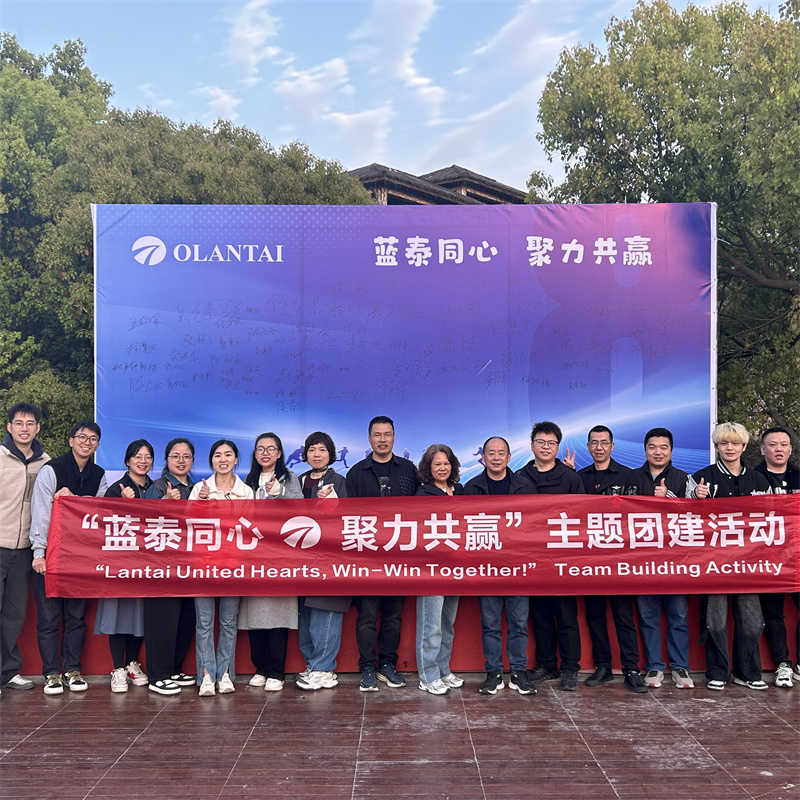
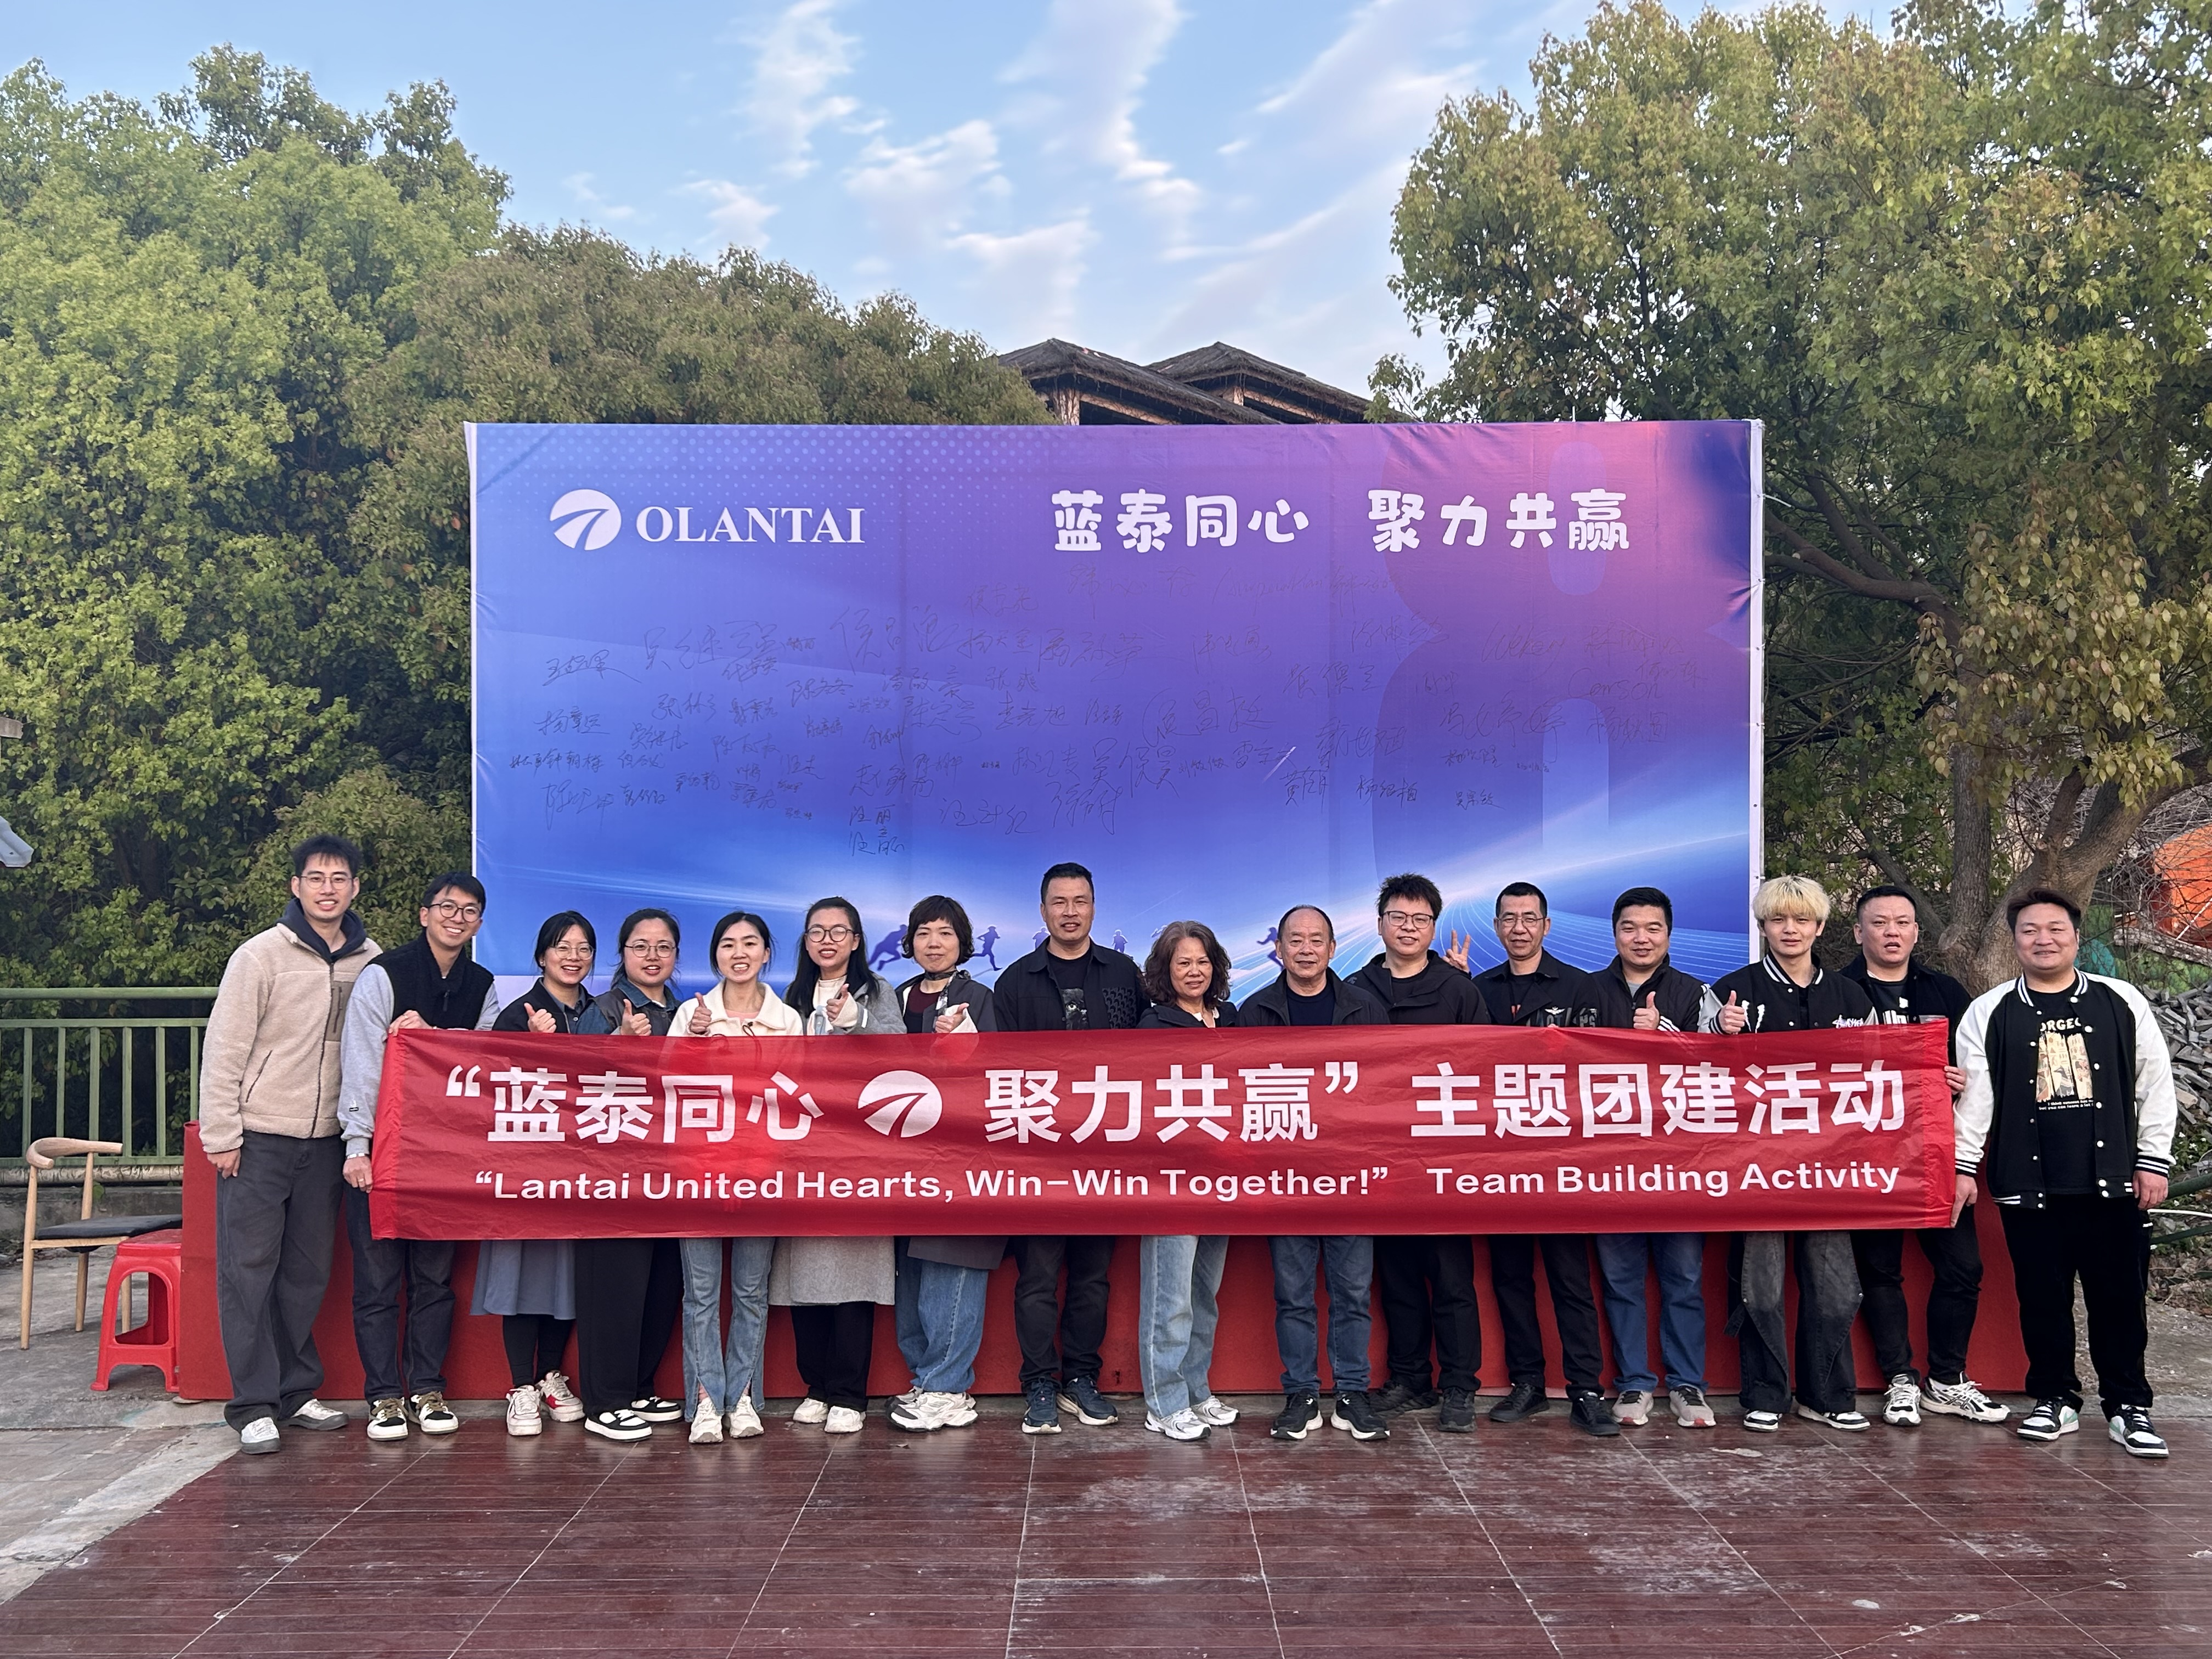
Fourteen years ago, Zhejiang Lantai Paper Product Co., Ltd. began as a modest label manufacturer serving regional clients in Zhejiang Province. Today, we operate a 22,636 square meter production facility with 65 employees, supplying custom thermal labels, boarding passes, baggage tags, and RFID solutions to businesses across North America, Europe, Asia, and beyond. Our evolution from local supplier to global OEM partner reflects a broader industry trend—and offers valuable insights for businesses seeking reliable private label manufacturing partnerships.
The Growing Demand for Private Label Label Programs
Private label programs have transformed from a cost-saving strategy to a core brand-building tool. In retail and logistics, branded labels serve as touchpoints that reinforce customer recognition, communicate quality standards, and differentiate offerings in crowded marketplaces. For businesses across industries, having control over label design, specification, and supply chain has become a competitive necessity.
This shift has created substantial demand for full-service OEM label manufacturers capable of delivering not just products, but comprehensive labeling solutions. At OLANTAI, we have structured our entire operation around meeting this need—combining manufacturing scale with the flexibility and responsiveness that private label programs require.
What Comprehensive OEM Label Manufacturing Looks Like
Our OEM services begin with collaborative product development. Clients work directly with our technical team to define specifications including label dimensions, material composition, adhesive properties, and pre-printed branding elements. Whether the requirement is standard 4x6 shipping labels with custom branding, specialized pharmacy vial labels with precise sizing, or durable aviation boarding passes with security features, our engineering team translates requirements into production-ready specifications.
Quality assurance is embedded throughout our process. Our facility maintains SGS certification, and our 5-person QA/QC team conducts material inspections, in-process monitoring, and finished goods testing. This systematic approach has enabled us to achieve a 98.5% on-time dispatch rate—a metric that directly supports our clients' ability to meet their own delivery commitments.
Inside Our Production Capabilities
Our 22,636 square meter facility houses advanced production equipment for thermal label coating, precision slitting, and high-speed rewinding. This scale enables us to handle bulk orders while maintaining the flexibility to accommodate smaller custom runs. Our product portfolio spans multiple categories: blank and pre-printed thermal labels for desktop and portable printers; specialized aviation labels including boarding passes and baggage tags; pharmaceutical labels with waterproof and prescription-ready features; and A4 self-adhesive sheets for office and retail applications.
The diversity of our product range reflects our commitment to serving varied industry needs. Aviation clients require labels that withstand handling stress and environmental exposure. Pharmaceutical clients need labels that comply with regulatory standards for readability and durability. E-commerce clients prioritize cost-effective, high-volume solutions that integrate seamlessly with automated fulfillment systems. Our manufacturing infrastructure is designed to deliver on all of these requirements simultaneously.
Industries We Serve: From Aviation to Healthcare
Our aviation product line—boarding passes and baggage tags—represents one of our most technically demanding categories. These products must meet strict industry standards for durability, readability, and security while being produced in high volumes to serve airline and airport clients. Our experience in this sector has refined our capabilities in precision printing and quality control, capabilities that translate directly to excellence across all our product categories.
In healthcare, our custom waterproof pharmacy vial labels address the critical need for accurate medication identification in challenging storage conditions. These labels must remain legible in refrigerated environments, resist moisture from condensation, and adhere reliably to glass and plastic vial surfaces. Our pharmaceutical clients rely on these products to support patient safety and regulatory compliance.
Building Long-Term Partnerships Through Service Excellence
Beyond manufacturing, our OEM partnerships are built on responsive communication and reliable execution. Our sub-3-hour response time ensures that client inquiries receive prompt attention, while our flexible minimum order quantities accommodate businesses at various scales of operation. Whether a client needs a small sample batch for product testing or a large production run for seasonal demand, our team scales to meet the requirement.
Conclusion
The journey from local supplier to global OEM partner requires more than production capacity—it demands consistent quality, responsive service, and the ability to adapt to evolving client needs. At OLANTAI, our 14-year track record demonstrates our commitment to these principles. For businesses seeking a reliable private label label manufacturing partner, we offer the combination of scale, expertise, and service that transforms supplier relationships into competitive advantages.
Precision Meets Compliance:
How OLANTAI Engineers Pharmaceutical Labels for Global Healthcare Markets
The pharmaceutical industry operates under some of the most stringent labeling requirements in the world. A label on a medicine vial is not merely an identifier—it is a critical safety component that ensures proper medication administration, tracks batch information for recalls, and maintains chain-of-custody documentation throughout the supply chain. At OLANTAI, we have dedicated years of specialized research and manufacturing refinement to develop pharmaceutical labels that meet and exceed the demanding standards of global healthcare markets.
Our OEM Custom Waterproof Pharmacy Vial Label represents the culmination of this focused effort—a product engineered from the substrate up to perform flawlessly in the challenging environments where pharmaceutical labels must operate. From hospital pharmacies to clinical research facilities, from regional distributors to global pharmaceutical manufacturers, our labels serve as the silent guardians of medication safety and traceability.
Understanding the Unique Challenges of Pharmaceutical Labeling
Pharmaceutical labels face environmental stresses that would compromise standard adhesive products. In hospital pharmacy settings, labels must withstand continuous exposure to refrigeration temperatures as low as -20°C, where conventional adhesives lose tack and paper substrates become brittle. During compounding and preparation, labels may encounter alcohol wipes, sterilization solutions, and other chemicals that can degrade standard printing and cause barcode readability failures.
The consequences of label failure in pharmaceutical applications extend far beyond operational inconvenience. A smudged barcode on a chemotherapy vial can delay critical treatment. A detached label on a compounded medication can create confusion about dosage and administration. For pharmaceutical manufacturers, label failures can trigger costly recalls, regulatory scrutiny, and reputational damage. These high-stakes requirements have shaped every aspect of our pharmaceutical label development process.
Substrate Engineering: The Foundation of Pharmaceutical Label Performance
The journey of a OLANTAI pharmaceutical label begins with careful substrate selection. Our thermal label paper is specifically formulated for pharmaceutical applications, with a thickness range of 0.1-0.12mm that provides the optimal balance of durability and conformability for vial application. Unlike standard thermal papers that prioritize cost over performance, our pharmaceutical-grade substrates incorporate moisture-resistant barriers and chemical stabilizers that prevent degradation in clinical environments.
The thermal coating technology we employ represents a significant advancement over conventional direct thermal products. Our proprietary coating formulation maintains thermal sensitivity for crisp, high-contrast printing while providing enhanced resistance to environmental factors that cause standard thermal prints to fade. This dual-functionality coating is the result of extensive R&D collaboration between our material scientists and pharmaceutical industry partners who provided real-world performance feedback from clinical settings.
Adhesive Science: Ensuring Permanent Bond Under Clinical Conditions
The adhesive layer of a pharmaceutical label is where engineering meets biology. Our waterproof adhesive formulation is designed to maintain strong bonding across the temperature extremes encountered in pharmaceutical storage and handling. From room temperature dispensing to refrigerated storage at 2-8°C, and even to freezer conditions at -20°C, our adhesive maintains consistent tack and peel strength.
Equally important is the adhesive's resistance to common clinical chemicals. During our development process, we subjected adhesive samples to extended exposure with 70% isopropyl alcohol, povidone-iodine solution, and other sterilants commonly used in pharmacy and clinical settings. Only formulations that demonstrated less than 5% degradation in bond strength after 24-hour exposure were considered for production. This rigorous screening ensures that our labels remain securely attached throughout the medication lifecycle, from dispensing through administration.
Print Technology and Barcode Reliability
Barcode readability is non-negotiable in pharmaceutical applications. A failed barcode scan can delay medication administration, trigger manual verification workflows, and introduce opportunities for human error. Our pharmaceutical labels are optimized for compatibility with the thermal printers commonly deployed in hospital pharmacies and pharmaceutical manufacturing facilities, ensuring consistent print quality and barcode readability across diverse equipment.
We offer multiple printing options to meet varying client needs. UV printing provides exceptional durability and chemical resistance for applications where labels face harsh environmental exposure. Silk-screen printing delivers precise color matching for brand consistency across product lines. Digital printing enables rapid turnaround for custom designs and short-run production. Regardless of the printing method selected, every label undergoes barcode verification testing using ISO-compliant scanners to confirm readability before shipment.
Customization and Regulatory Compliance
Pharmaceutical labeling requirements vary significantly across markets and applications. Our OEM customization capabilities enable clients to specify exact dimensions, shapes, and configurations to match their vial formats and dispensing equipment. Color coding supports visual identification protocols, with full CMYK and Pantone color matching available to ensure brand and safety color consistency.
Regulatory compliance is woven into every aspect of our pharmaceutical label production. Our facility maintains ISO9001, ISO14001, and OHSAS18001 certifications, providing clients with documented quality management systems. For European markets, our products comply with EN495 standards and REACH regulations, ensuring that materials meet the strict chemical safety requirements for products used in healthcare settings. These certifications are not merely credentials—they represent the systematic processes that govern our material sourcing, production controls, and quality verification.
Quality Assurance: The OLANTAI Standard
Our quality assurance program for pharmaceutical labels reflects the critical nature of the applications they serve. Each production batch undergoes comprehensive testing including adhesion strength measurement, water resistance verification, barcode readability confirmation, and dimensional accuracy inspection. Our five-person QA/QC team maintains detailed inspection records for every lot, providing full traceability and supporting our clients' own quality documentation requirements.
This quality-first approach has contributed to our 98.5% on-time dispatch rate and 26% reorder rate—metrics that reflect not just operational efficiency, but the trust that pharmaceutical clients place in our products. When a hospital pharmacy or pharmaceutical manufacturer reorders from OLANTAI, they are confirming that our labels have performed reliably in their critical applications.
Applications Across the Healthcare Spectrum
Our pharmaceutical labels serve diverse applications throughout the healthcare industry. Hospital pharmacies rely on our waterproof vial labels for unit-dose packaging, IV admixture labeling, and compounded medication identification. Pharmaceutical manufacturers use our labels for clinical trial materials, where precise batch tracking and chain-of-custody documentation are essential. Research laboratories depend on our labels for specimen identification in studies where sample integrity directly impacts data validity.
In each of these applications, the common thread is the need for labels that perform without fail in demanding environments. Our clients do not select OLANTAI labels because they are the least expensive option—they select them because our engineering investment in substrate technology, adhesive science, and quality assurance delivers the reliability that healthcare applications demand.
Conclusion
The pharmaceutical label market demands products that go far beyond basic identification. At OLANTAI, we have built our pharmaceutical label capabilities on a foundation of material science, adhesive engineering, and uncompromising quality control. Our OEM Custom Waterproof Pharmacy Vial Label embodies these principles, delivering the performance that healthcare professionals and pharmaceutical manufacturers require to maintain patient safety and regulatory compliance.
As global healthcare continues to evolve—with increasing emphasis on personalized medicine, decentralized pharmacy services, and stringent regulatory oversight—the demand for pharmaceutical labels that can meet these challenges will only grow. We remain committed to advancing our technology and capabilities to serve this critical market, ensuring that every label we produce contributes to the safe and effective delivery of healthcare worldwide.
About OLANTAI
Founded in 2010, OLANTAI is a leading manufacturer of thermal labels, boarding passes, baggage tags, RFID labels, and specialty paper products. With ISO9001, ISO14001, OHSAS18001, EN495, and REACH certifications, our 22,636 square meter facility and 65-person team—including 5 dedicated QA/QC inspectors—deliver OEM and private label solutions to clients across aviation, healthcare, retail, and logistics sectors worldwide.